Sewage or grinder pumps move raw sewage and unwanted water away from the home. Our pre-plumbed packages make selecting and installing the right equipment easy.
Flint & Walling offers a selection of reliable water pumps and systems designed to help you maintain lush lawns and vibrant gardens. Browse our catalog to find the product that suits your needs.
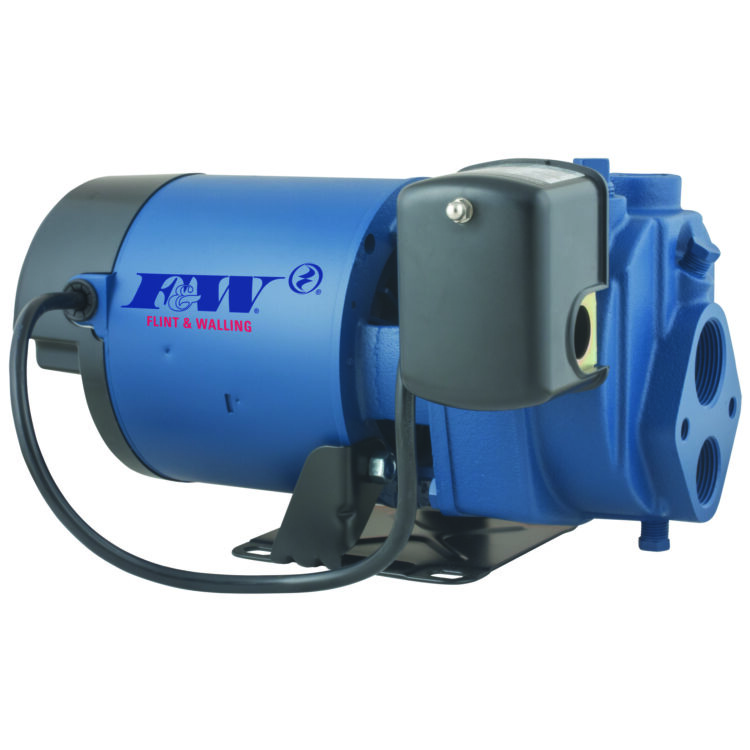
Flint & Walling has a selection of submersible pumps and jet pumps designed with robust components to deliver superior performance across a range of applications.
Elevate the appearance of parks, golf courses, and residential communities with decorative fountain pumps that combine stunning visual displays with continuous water circulation for improved water quality and aesthetics.
During storms, excess water can lead to flooding, pollution, and damage. We offer a range of pumps, containers, and controls to manage your stormwater effectively.
Designed for cleaning and maintaining tankless water heaters, the Scale Removal System efficiently circulates descaling solutions to remove mineral deposits and scale buildup. Regular flushing helps improve system efficiency, maintain consistent hot water performance, and extend equipment life.
Remove condensation from air conditioning equipment, condensing furnaces, dehumidifiers, ice makers, water coolers, and refrigeration systems when gravity flow is not an option.
From pressure boosting to maintaining constant pressure or regulating pressure, our range of water pressure booster pumps offer tailored solutions to tackle any challenge effectively.
Our tailored products ensure livestock comfort by providing reliable water supply solutions specifically designed for use in poultry houses and livestock environments
A car wash cannot perform efficiently with low water pressure. These products are a great solution for these applications where you need high and consistent pressure.
Designed for the demanding needs of commercial applications, these pump systems and packaged solutions provide reliable water and wastewater management, helping facility managers maintain uninterrupted operations and long-term peace of mind.
Our hazardous duty explosion-proof effluent and sewage pumps are rated for Class 1, Division 1, Groups C & D or Class 1, Zone 1, Groups IIA & IIB. Every pump is submerged in water and tested at the factory to ensure that it performs as expected when you receive it.
Designed for residential and community wastewater collection, low pressure sewer systems provide dependable wastewater transport, offering flexibility for difficult terrain, longer distances, and expanding developments.
Engineered for the demands of municipal operations, these pumping systems deliver dependable wastewater and stormwater management to support growing communities and critical public infrastructure.
A debate in the submersible wastewater pump industry has been regarding which is better – an oil-filled motor or an air-filled motor. An oil-filled pump is defined as having the motor cavity filled with oil, usually to cover the upper bearing and windings. An air-filled pump is one that does not use oil to fill the motor cavity.
Why Zoeller predominately chooses an oil-filled motor to provide the most dependable product to our customers.
According to the SWPA (Submersible Wastewater Pump Association) handbook, “With a submersible pump, heat transfer is accomplished by direct conduction to the relatively constant temperature fluid being pumped. This more efficient heat transfer method, versus a dry-mounted pump, results in a lower operating temperature for the motor and its internal components, and it helps extend the life of the motor.” Let’s take the above quote one step further. If it is beneficial to submerge the pump in water for better heat transfer, then why not submerge the stator in oil for the same reason? Oil-filled motors lower the winding temperature through extra heat transfer away from the stator, to the housings, and then out into the liquid.
We all know heat has a negative impact on electrical components, so any effort to lower the operating temperature inside the pump will yield a longer-lasting product. Other advantages include a more uniform winding temperature, which eliminates destructive hot spots in the motor, and permanently lubricated bearings and seals, which will extend the product life due to a lower risk of overheating. Without the oil to provide constant heat dissipation from the motor, the biggest disadvantage to an air-filled pump is the higher risk to overheat and burn up the motor. This will shorten the product life and require complete replacement of the pump rather than a simple repair.